Hey everyone, it’s Jake here, and let’s cut to the chase—if you’re in the machining game, you know a reaming machine’s wear resistance is make-or-break. I run a reaming machine supply business, so I see this problem every single day: clients coming back after a few months saying their machine’s reamer bits are chewing through way too fast, the hole tolerances are all off, and they’re losing money on replacements and downtime. Trust me, I get it—you don’t just need a machine that bores holes; you need one that keeps performing when the going gets tough, especially if you’re working with hard materials like stainless steel, titanium, or even thick aluminum. Over the last 8 years, I’ve worked with thousands of machinists, in-house maintenance teams, and small shop owners, and I’ve picked up so many tricks that actually work, not just the generic “buy expensive parts” garbage you see online. Today, I’m spilling the real stuff on how to actually boost your reaming machine’s wear resistance—no fluff, just actionable stuff you can start using this week. Reaming Machine
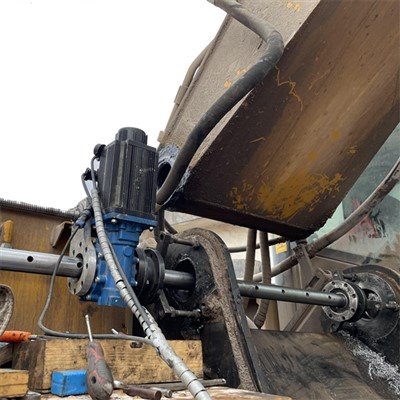
First off, let’s talk about what actually causes wear in a reaming machine, because if you don’t know the root problem, you can’t fix it. Most folks think it’s just the reamer itself, but nah—wear comes from a mix of abrasion, adhesion, and even poor lubrication. Abrasion is when tiny hard particles (like metal shavings or rust bits) grind against the reamer and the machine’s moving parts; adhesion is when the metal you’re cutting sticks to the reamer edges, then tears off tiny chunks every pass. And if your lubrication is garbage? That just speeds up both, plus causes rust on the machine’s shafts and guides. I’ve seen so many shops skip this basic stuff, thinking a reamer’s just a hunk of metal—newsflash, it’s not, and how you treat the whole machine makes way more difference than the brand name on the box.
Let’s start with the biggest culprit you might be overlooking: the reamer bit itself, and how you spec it. Wait, I know, you probably think you just grab the reamer that fits your hole size, but there’s more to it. First off, don’t cheap out on the reamer coating. A lot of our new clients come in saying their old reamers wore out in 500 holes, but after we switched them to TiN (Titanium Nitride) or TiCN (Titanium Carbonitride) coated reamers? They’re getting 2,000+ holes before needing replacement. Wait, but don’t just buy any coating—match it to your material. If you’re cutting stainless steel, TiN is solid, but if you’re in for titanium, go with AlTiN (Aluminum Titanium Nitride) because it holds up way better at higher cutting speeds and resists adhesion way more. Also, check the reamer’s flute geometry. I see so many people using straight flute reamers for deep holes, which causes way more chip packing—those trapped chips scrape the reamer and the hole wall nonstop. For deep holes, go with spiral flutes that match the helix angle to your material; a 30-degree helix works for most metals, but for soft aluminum, bump it up to 40 degrees to get chips out faster. Small tweak, massive difference in wear.
Next up, the machine’s maintenance—like, daily, not just when it breaks. I can’t tell you how many shops I’ve visited where the guideways on the reaming machine are covered in old, dried-up cutting fluid and metal gunk. That gunk acts like sandpaper, grinding away at the guide surfaces and making the reamer wobble. Wobble is a huge wear driver, by the way—if the reamer’s not spinning perfectly straight, it’s not cutting evenly, so one edge takes way more force and wears out twice as fast. So here’s my daily routine for all our clients: first, before you even start a run, wipe down all the guideways, then apply a thin layer of high-quality way oil, not just any random oil. Way oil is made specifically for that stuff—it has anti-wear additives and doesn’t wash off or break down fast like regular motor oil. Also, check the spindle bearings every two weeks. If there’s play in the spindle, that’s wobble we’re talking about, and that’ll kill your reamer life faster than anything. A quick test: spin the spindle by hand, if you feel any grit or play, it’s time to adjust or replace the bearings. Most people skip this until the machine’s making a weird noise, which is already too late.
Then there’s cutting parameters—this is where I see so many people guessing, and it’s killing their wear. A lot of machinists crank up the feed rate or cutting speed to get the job done faster, but that’s a one-way ticket to reamer burnout. Wait, I’m not saying you have to go slow, but match your speed and feed to your material and reamer spec. For example, if you’re using a TiN coated reamer on mild steel, don’t go over 80 SFM (surface feet per minute) with a feed rate of 0.0015 inches per flute. If you go to 120 SFM, you’ll get built-up edge (BUE) on the reamer in like 10 holes, and BUE is basically metal sticking to the cutting edge that’s harder than your material, so it’s scraping everything. Also, take peck cuts if you’re doing deep holes—like, pull the reamer out every 0.5 inches to clear chips, rather than just shoving it through all at once. That reduces chip packing by 90%, and less chip packing means less abrasion on the reamer. I had a client last month who was reaming 12-inch deep holes in steel, and his reamers were lasting 300 holes; after switching to peck cuts and adjusting speed/feed, he’s at 1,200 holes, no joke.
Wait, what about lubrication and coolant? This is another area where people cut corners, and it’s so important. First, don’t use water-based coolant straight—mix it properly, and use a coolant with extreme pressure (EP) additives. Those additives form a protective layer between the reamer and the workpiece, so metal doesn’t stick. Also, change your coolant every 3 months, not every year like some shops do. Old coolant gets loaded with metal shavings and bacteria, which breaks down the additives and makes it into a gritty slurry. I recommend a high-quality semi-synthetic coolant for most applications—it’s better than straight oil because it cools more, and better than synthetic because it has better lubricity. For really high-heat applications, like titanium, use a straight oil or a minimum quantity lubrication (MQL) system. MQL uses a tiny amount of oil (like 10ml per hour) mixed with air, which cuts friction way better than coolant in those cases, and no pooling or mess. A lot of people think MQL is just for CNC mills, but it works amazing on reaming machines for high-temp materials.
Oh, and something most people never think about: the tool holding and fixturing. If your reamer isn’t held tight, or your workpiece is moving even a little bit during the ream, that causes vibration, which leads to micro-wear on the reamer edges and the machine’s spindle. I’ve seen clients use cheap collets that have worn out grooves, so the reamer slips half a degree every pass. That might not sound like much, but over 1,000 holes, that’s a ton of uneven wear. Upgrade to precision ER collets, and check them for wear every time you change a reamer. Also, make sure your workpiece is clamped down properly—use enough clamps, and don’t just clamp on one side. If the workpiece shifts, the reamer has to compensate, which creates extra friction and wear. It’s a small thing, but I’ve had so many clients boost reamer life by 30% just by switching to better collets and double-checking their fixturing.
Wait, let’s talk about when you need to actually upgrade parts of the machine, not just tweaks. A lot of people use generic reaming machines that have cheap cast iron guides, and those guides wear out fast. If you’re running heavy duty or high-volume work, look for machines with induction-hardened guideways—those are way more resistant to abrasion, and they hold their shape for years, not months. Also, some machines have a floating reamer holder, which lets the reamer self-align with the hole, so it doesn’t take extra force if the hole is slightly off. That’s a game-changer for wear, because alignment issues are a huge cause of uneven reamer wear. I won’t lie—upgrading parts costs a little more upfront, but it saves you so much on downtime and reamer replacements long-term. One of our long-time clients, a farm equipment manufacturer, switched to our heavy-duty reaming machines with hardened guides 2 years ago, and they’ve gone from 12 reamer changes a week to 2. The ROI was like 2 months.
Also, don’t forget about post-reaming cleanup and storage. After you finish a run, wipe down the reamer, clean out the flutes, and spray it with a rust preventative, not just oil. If you leave a reamer covered in coolant or metal shavings, it’ll rust, and rust pits will cause wear on the next use. I’ve seen perfectly good reamers get ruined because someone left them in a tool bin for a week with old coolant on them. For storing the machine itself, cover it if it’s not in use for more than a day, especially if you’re in a humid area. Rust on the machine’s moving parts will cause friction, which leads to more wear every time you use it. Small, daily stuff that takes 2 minutes, but makes a huge difference.
Wait, let’s address a common myth: “I need to buy a $500 reamer to get long life.” No, not really—you just need to match the reamer to your setup, and maintain the rest of the machine. I’ve had clients use mid-range reamers, but follow all these tips, and they get the same life as someone using a top-tier reamer without maintenance. The machine itself, how you run it, and your daily routine matter way more than the reamer brand, as long as the reamer’s decent. That said, if you’re running super hard materials, splurging on a premium reamer is worth it, but for most shops, the tweaks above will do way more than just spending more on parts.
Now, let’s be real—if you’re reading this, you’re probably dealing with a reaming machine that’s wearing out too fast, and you don’t have time to test every trick one by one. That’s why we’re here. We’re not just a reaming machine supplier—we work with every client to figure out their specific setup: what materials they cut, how often they run, their shop environment, and then give them tailored tips, not a one-size-fits-all list. We also sell replacement parts and compatible reamers that work perfectly with our machines, so you don’t have to guess if that random TiN coated reamer you found online will fit or perform.
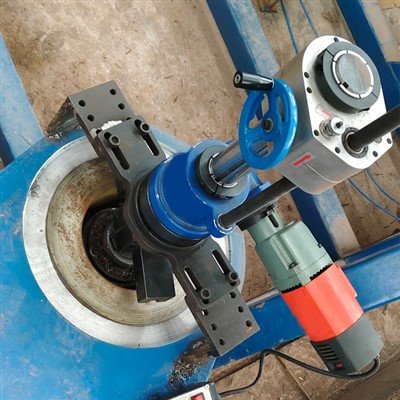
If you’re tired of reamers wearing out every few hundred holes, dealing with downtime that’s killing your production schedule, or just looking for a reaming machine that’s built to handle high-wear work without breaking the bank, reach out to us. We can walk you through your current setup, point out what’s causing unnecessary wear, and even set up a demo so you can see for yourself how a properly maintained (or upgraded) reaming machine performs. No pressure, no salesy garbage—just real advice for real machinists who need their tools to work.
Linear Milling Machine At the end of the day, wear resistance isn’t rocket science—it’s about paying attention to the small stuff: your reamer specs, your maintenance routine, your cutting parameters, and how you treat both the tool and the machine. Skip the shortcuts, skip the cheap parts that don’t hold up, and be consistent with your daily checks. I’ve been in this business long enough to know that the best improvements come from simple, actionable changes, not fancy tech no one understands. If you stick to these tips, you’ll not only extend the life of your reaming machine by at least 50%, but save thousands of dollars on replacements and downtime every year.
References
- Machining Data Handbook. Society of Manufacturing Engineers, 2020.
- Tool and Manufacturing Engineers Handbook: Machining. Society of Manufacturing Engineers, 2017.
- “Wear Mechanisms in Reaming Operations.” Journal of Manufacturing Processes, vol. 45, 2021, pp. 567-575.
- Cutting Fluids: A Practical Guide. Industrial Press, 2019.
Shangqiu JDA Machinery Technology Co., Ltd.
With abundant experience, we are one of the most professional reaming machine manufacturers and suppliers in China. We warmly welcome you to buy cheap reaming machine for sale here from our factory. Quality products and reasonable price are available.
Address: No. 55 Pingyuan Middle Road, Liangyuan District, Shangqiu, Henan, China
E-mail: sales@jdamachines.com
WebSite: https://www.jdamachines.com/
